
What causes inconsistent torque on a bottle capping machine?
Time : Oct 02, 2026
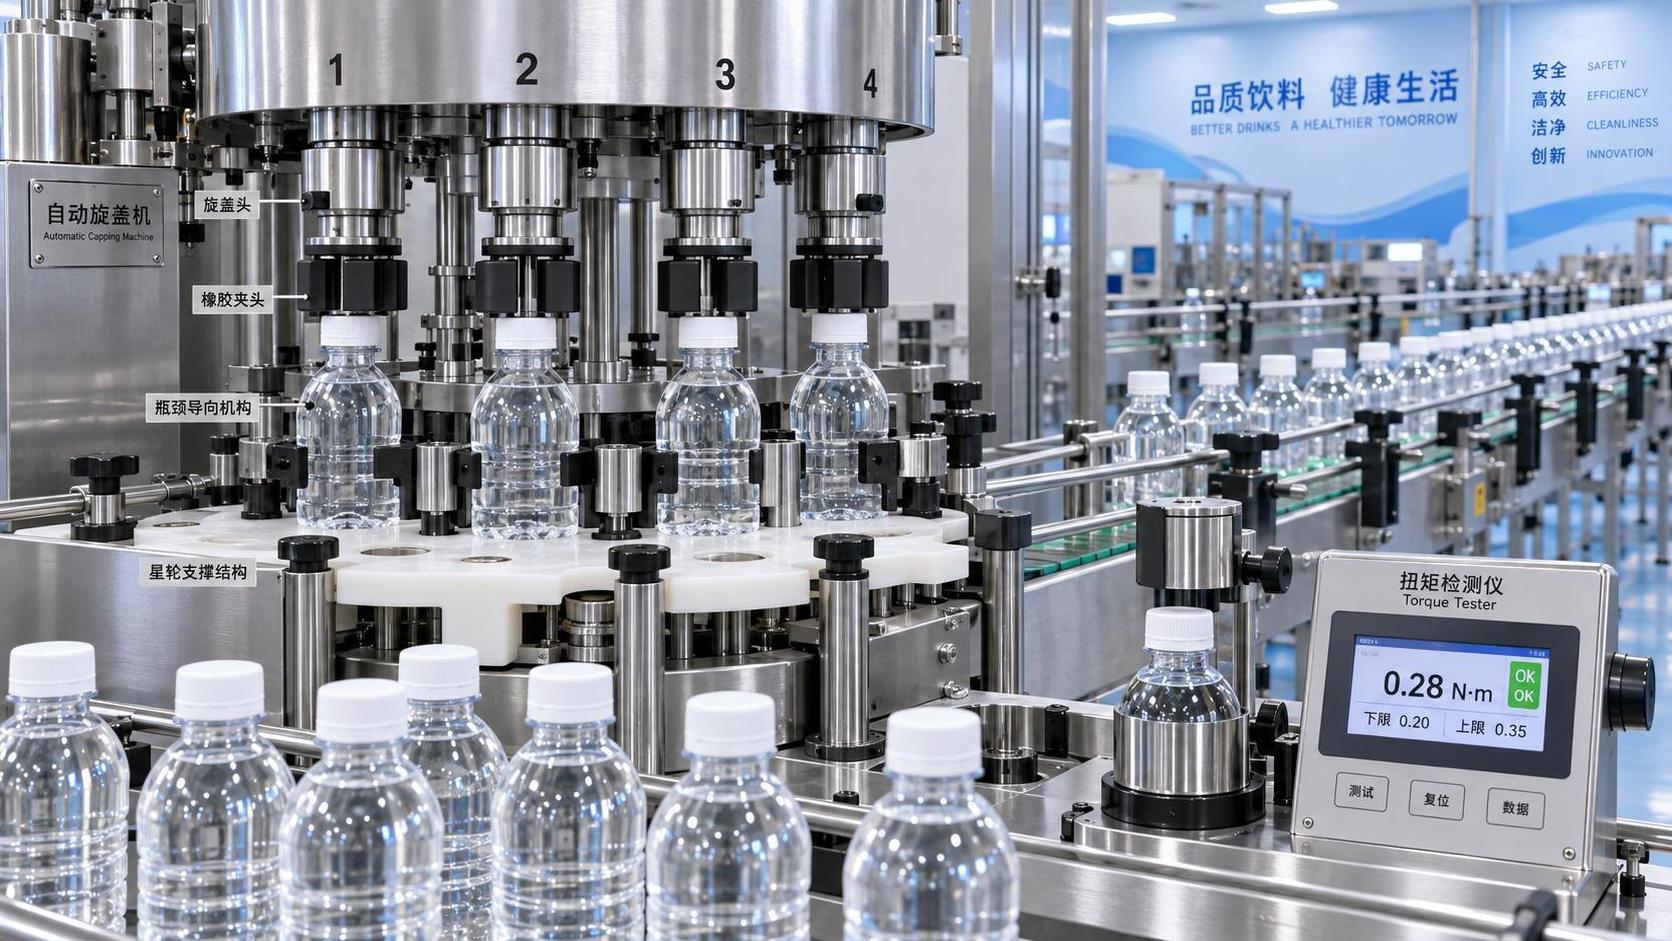
A bottle line may run smoothly for several minutes and then begin producing a mix of loose caps, over-tightened closures, scuffed threads, or containers that fail a downstream leak check. Inconsistent torque is rarely caused by one adjustment alone. On a Bottle Capping Machine, torque variation usually comes from changes in cap presentation, bottle support, spindle or chuck condition, pneumatic stability, clutch behavior, or an incorrect relationship between line speed and capping-head speed.
The fastest way to restore control is to determine whether the variation follows a pattern. Check whether it occurs on one capping head, one bottle lane, one closure batch, only at higher speeds, or randomly across the machine. That distinction separates a localized mechanical fault from an air supply, setup, or incoming-material issue. Avoid increasing torque settings before identifying the source; a higher setting can hide low-torque failures while creating damaged caps and distorted bottle finishes elsewhere.
Start with the torque pattern, not the torque setting
Before dismantling parts, collect a small but meaningful set of samples from normal production. Measure applied torque with a calibrated torque tester after capping, and note the head number, cap type, bottle type, time of collection, and line speed. If applicable, also record removal torque after the specified dwell period, because application torque and removal torque are not always the same.
A useful first observation is whether the deviation is repeatable:
- One head consistently applies lower or higher torque: inspect that head’s chuck, spindle, clutch, bearings, vertical travel, or pneumatic drive.
- All heads drift together: investigate supply air, regulator performance, machine speed changes, bottle handling, or a change in caps or containers.
- Variation increases at higher output: look for cap-feed timing, insufficient bottle stabilization, slipping drive components, or inadequate capping dwell time.
- Random high and low values: check cap dimensions, liner condition, cross-threading, intermittent air-pressure loss, loose fasteners, and vibration.
Technicians sometimes focus immediately on the final torque reading. The more useful question is what happened during cap engagement. A cap that arrives tilted, begins on a damaged thread, or is spun before the bottle is fully centered can produce an acceptable-looking closure with an unreliable torque result.
Caps and bottle finishes can change the result before the capper touches them
Closure torque depends on the interface between the cap, the bottle finish, and any liner or sealing feature inside the closure. A machine can be mechanically sound yet show unstable readings when incoming packaging materials vary. This is especially important after a new delivery of closures, a bottle mold change, or a switch between products using visually similar components.
Closure-related causes
Check for inconsistent cap height, skirt diameter, thread profile, bridge condition, liner placement, liner thickness, or molded flash. A cap with a displaced liner may resist tightening differently from the rest of the batch. Caps with oil, dust, moisture, or product residue can also slip in the capping chuck or alter friction at the bottle finish.
Cap feeding deserves close attention. Centrifugal sorters, elevators, chutes, and cap rails can create scuffs, deformation, or poor orientation before the closure reaches the pick-off point. A cap that drops onto the bottle off-center may be corrected by the capping head, but the correction consumes part of the available capping cycle and can lead to cross-threading or erratic torque.
Bottle-related causes
Inspect the bottle neck finish for ovality, incomplete threads, flash, contamination, and damage caused by upstream handling. Lightweight bottles can flex under capping load, particularly when neck guides or base support are poorly adjusted. That flex changes the effective torque transferred to the closure. A bottle may also rotate in the starwheel pocket or on the conveyor rather than holding firm against the torque applied by the capping head.
When a new bottle or cap is introduced, confirm that the machine’s contact tooling matches the component. A chuck designed for one closure geometry may grip another closure only at a narrow edge. It can slip intermittently, mark the cap, or apply uneven force even when the clutch is set correctly.
Inspect the cap application path
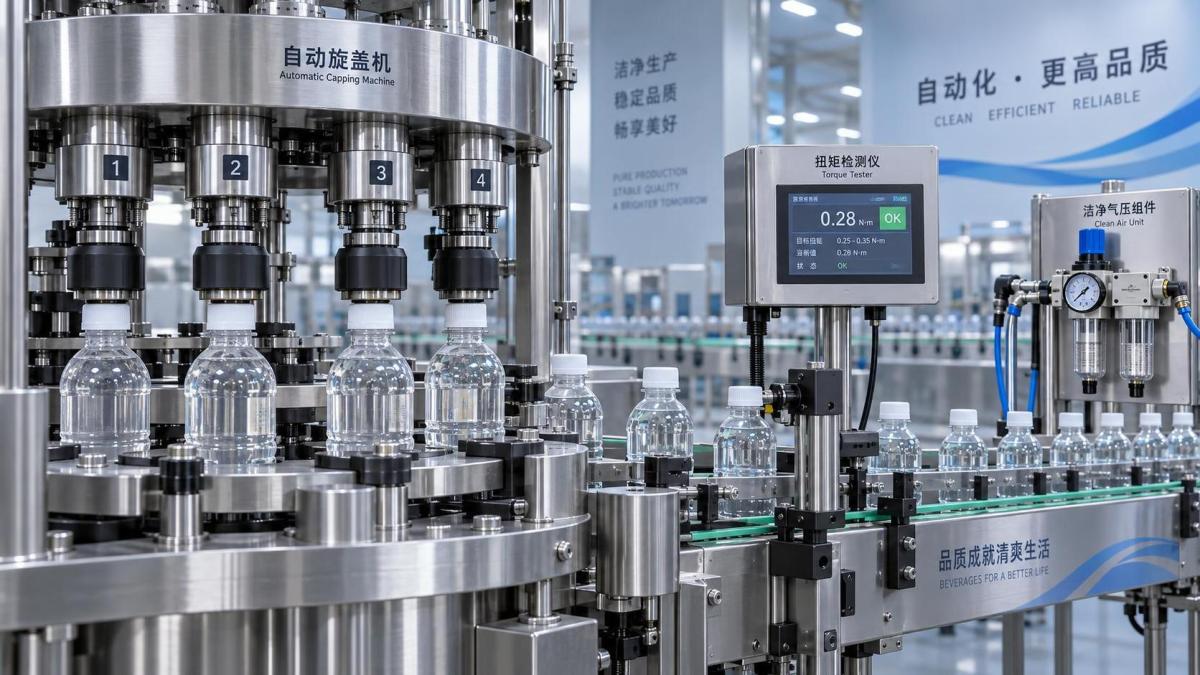
The cap must be presented squarely, held correctly, started on the thread, and tightened while the bottle remains stable. A defect at any point in that path can look like a torque-control problem.
First observe the cap just before tightening. It should be seated on the bottle finish without a visible lean. The bottle should be centered under the capping head, with enough support beneath it to resist downward force and rotational load. Check guide rails, starwheel pockets, neck guides, bottle plates, and lift mechanisms for excessive clearance or wear. Loose guides allow the bottle to move laterally; overly tight guides can drag the bottle and interfere with smooth rotation.
Then inspect the vertical position of the capping head. If it reaches the cap too early, it may compress or bind the closure before the thread has started correctly. If it contacts too late, the head may not have enough time or travel to complete the capping cycle at the intended speed. The correct setting depends on container height, closure design, and machine configuration, so make adjustments in controlled increments and verify them with actual torque readings rather than visual judgment alone.
On multi-head equipment, compare head height and spring or pressure settings across all stations. A single head that sits slightly higher or lower than the others often produces a repeatable outlier. Mark the problematic head, stop the machine safely, and inspect it against a known-good station rather than adjusting every head at once.
Worn or contaminated chucks are a frequent source of uneven torque
Chucks, capping discs, rubber inserts, and gripping liners transfer rotation from the machine to the closure. Their condition directly affects repeatability. Hardened rubber, glazed surfaces, embedded debris, cracked inserts, and uneven wear reduce grip. The result may be low application torque, intermittent cap slip, or torque readings that fluctuate despite unchanged settings.
Examine the contact surface under good lighting. Look for polished areas, tearing, swelling, missing material, and residue from caps or product. Clean only with materials compatible with the chuck and closure; aggressive solvents can damage elastomer components or leave a slippery surface. After cleaning, allow the components to dry fully before testing.
Also check whether the chuck is properly retained and concentric. A loose chuck can wobble, contact the cap unevenly, and leave scuffing concentrated on one side of the closure. If the machine uses magnetic or quick-change tooling, confirm that the seating surfaces are clean and fully engaged.
Do not assume all four heads wear at the same rate. One station may handle more load because of a minor alignment difference, or it may be exposed to more product splash. Replace worn parts according to condition and machine guidance, ideally as a matched set when different wear levels would create avoidable variation between heads.
Pneumatic instability affects both force and timing
Many capping systems use compressed air for head lift, bottle lifting, clutch actuation, or other motion. Pressure that looks acceptable on a static gauge may still be unstable while the line is running. A regulator can lag, a filter can restrict flow, a hose can leak under movement, or another air-consuming device on the line can cause a pressure drop during peak demand.
Watch the regulator while several heads are cycling. If pressure fluctuates at the same time torque readings become inconsistent, trace the supply upstream. Drain water from air preparation units, inspect filters, verify regulator operation, and listen for leaks around fittings, valves, cylinders, and flexible tubing. Moisture or oil carryover can also affect pneumatic valves and reduce consistent response.
Low pressure does not always create uniformly low torque. It may alter head engagement timing or bottle-lift force, leading to caps that are applied correctly on some cycles and poorly on others. A sticking solenoid valve or sluggish cylinder can create the same symptom on one station. Compare the movement speed and full-stroke position of each head or lift assembly during a slow jog cycle.
Check torque clutches, drive belts, and rotating components
Mechanical torque limiters and clutches protect caps and bottles from excessive tightening, but they require inspection. A clutch may be contaminated, incorrectly adjusted, worn internally, or slipping inconsistently as it heats during production. If torque falls after the machine has been running for some time, compare cold and warm behavior. Heat-related change can point to clutch friction surfaces, bearings, lubrication problems, or belt tension.
Drive belts and chains should be inspected for tension, wear, alignment, and contamination. A belt that slips only under load can cause brief loss of spindle speed that is difficult to see during normal operation. Check pulleys for looseness and worn keyways, and verify that couplings are secure. Unusual vibration, rhythmic noise, or a head that accelerates unevenly should be treated as diagnostic evidence, not merely a nuisance.
Bearings in capping spindles, gearboxes, or lift mechanisms can introduce drag or play. Excessive radial movement affects chuck alignment; rough rotation changes how torque is delivered. With the machine isolated according to site procedures, rotate and move components by hand where access permits. Compare suspect stations with a station known to operate normally.
Speed changes can expose an adjustment that seemed acceptable
A setting that works at a reduced commissioning speed may fail at normal production output. As conveyor speed rises, the capper has less time to settle the cap, engage the thread, and reach target torque. Bottle movement becomes more significant, especially with tall, lightweight, or partially filled containers.
Run a controlled comparison at a lower and then normal speed using the same bottles and caps. If consistency improves at low speed, inspect cap delivery timing, starwheel transfer, bottle support, and head synchronization before changing the torque setting. The issue may be insufficient engagement time rather than insufficient torque capacity.
Product fill level can matter as well. A nearly empty bottle may behave differently from a full bottle because the container has less mass and may be easier to rotate or lift. Changes in product temperature can alter bottle stiffness or closure-liner behavior. These conditions do not automatically require a different machine setting, but they should be considered when torque instability appears only on certain SKUs or production stages.
A practical fault-isolation sequence
When downtime is limited, isolate variables instead of making broad adjustments. Begin with a verified sample of bottles and caps, then test the machine at a stable moderate speed. Measure enough consecutive containers to identify whether a particular head is responsible. If one head is abnormal, swap only the removable chuck or insert with a known-good head where the design allows. If the fault moves with the chuck, the gripping component is the likely cause. If it remains at the same station, inspect the drive, clutch, pneumatic circuit, and vertical alignment for that station.
When all heads show variation, verify incoming materials and air supply before recalibrating every torque mechanism. Next, review bottle stability and cap-feed presentation. This order prevents a maintenance team from compensating for a material or handling problem with excessive mechanical settings.
Resetting the machine after repairs
After correcting a fault, do not return immediately to full output. Set the head height, guide position, and torque mechanism according to the closure and bottle being run. Produce a short controlled sample, measure torque across every head, and inspect caps for marks, tilt, thread damage, and tamper-band deformation. Then increase speed in stages while continuing to sample.
Equipment with several capping stations benefits from a documented head-by-head baseline. Record the closure type, container type, operating speed, air pressure, torque setting position, and measured range that is acceptable for the product’s packaging requirements. This does not replace formal quality procedures, but it gives maintenance personnel a practical reference when a later deviation appears.
Where production requires a multi-head automatic capper, accessible tooling and independently inspectable stations can shorten diagnosis. The ZFG-4 Fully Automatic 4-Head Capping Machine can be evaluated in terms of how its head arrangement, bottle handling, and capping adjustments fit the closure formats being used. Regardless of machine model, repeatable torque depends on keeping the cap, bottle, gripping tool, drive system, and air-assisted motions stable as one process rather than treating torque adjustment as an isolated control.
Persistent torque variation after checks of materials, tooling, alignment, pneumatic supply, and drive components may indicate internal clutch wear, control synchronization issues, or a mechanical condition that requires deeper service inspection. Continuing to run while compensating with higher torque settings risks masking the original fault and increasing closure or container damage.
Leave A Message
If you are interested in our products and want to know more details, please leave a message here, we will reply you as soon as we can.